Steel Structure Building Manufacturer

Loading

Jump To Your Operation Meat & Poultry Processing

A chilled meat plant and a frozen storage hall can share a site wall and share almost nothing else. One runs a daily washdown routine that attacks every untreated surface; the other lives or dies by whether a single thermal bridge stays dry. Design a food building as “a warehouse with panels” and the failures arrive in the first audit season: condensation on column heads, hygiene inspectors finding ledges nobody can clean, floors pitted by chemicals the frame specification never mentioned.

Food-chain buildings are decided by three regimes — temperature, hygiene and washdown — and each regime pushes back on the structure differently. Below: the four decisions we treat as non-negotiable, what each of the five common operations demands, and the projects behind it.

What a food & cold chain building must get right

Four decisions. Each one is expensive to revisit after fabrication.

1

Temperature zones decide the envelope — not the other way round

Chilled at 0–4 °C and frozen at −25 °C are different buildings wearing the same cladding. Panel thickness, vapour-barrier orientation, and where thermal breaks go are all fixed by the coldest zone — and by which side of the wall is wet. A vapour barrier on the wrong face does not insulate badly; it quietly rots the panel from inside over three winters.
2

Hygiene is a geometry problem before it is a coating problem

Auditors grade what they can see and reach: ledges where dust settles, joints harbouring residue, cavities nobody can access. We detail flush connections, coved junctions and cleanable interfaces as part of the frame design — because a retrofit “hygiene kit” of angle fillets and sealant beads is exactly what fails the next inspection.

3

Floors take the worst of both regimes

Washdown chemicals etch untreated concrete; forklift traffic works the joints until they lips; chilled rooms need slopes and drains that frozen rooms forbid. Floor specification is a process decision — we take the cleaning schedule and the traffic plan together, and the slab follows both. Fixing floor slope after the racking is installed is not a project; it is a closure.

4

Every door is an airlock waiting to be designed properly

Each opening between temperature zones is a thermal leak and a condensation seed. Fast-roll doors, air curtains and vestibule lobbies cost a fraction of the energy they save — but only if they are in the layout from the start. Squeezing a lobby in later means stealing it from racking, and the racking was drawn first.

Five operations, five different briefs

Each section below answers one operation. Find yours — or read all five to see how different they really are.

Meat & Poultry Processing

Daily washdown, ammonia on the steel, 3 °C rooms inside an ambient shell

A meat plant is two buildings in one: an ambient shell that carries the roof, and a chilled processing box inside it — with a washdown regime between them that runs every shift. Frames in this environment are specified for ammonia-rich and salt-washed atmospheres: galvanized or two-coat systems on all steel within the wet zone, because paint that survives a warehouse roof will not survive the second year above a kill floor. Drainage falls are engineered with the slab, not after it; the panel joints in process rooms are sealed and coved so the routine ends where the auditor starts.

Typical requirement set: processing rooms 3–8 °C · washdown-rated coatings · sealed coved joints · graded drainage · ceiling voids accessible for inspection.
Dairy & Beverage

Wet process, CIP routines and tank loads the slab must not argue with

Dairies and beverage plants combine a wet, acidic process floor with equipment that concentrates tons on four feet. Tank plinths and equipment reactions go into the foundation design from day one — the slab is a process document. CIP (clean-in-place) chemicals set the floor finish choice; roof ventilation sets how much of the humidity leaves instead of condensing on your purlins.

Typical requirement set: tank and equipment loads in the foundation brief · acid-resistant floor finish · CIP-compatible drainage · condensation control above wet process zones.
Fruit & Veg Packhouses

High humidity, ripening rooms, and a season that never pauses

Packhouses breathe: intake humidity, ripening rooms held at exact temperature bands, dispatch that cannot wait for the harvest to. The envelope must handle persistently high internal humidity — the failure mode is interstitial condensation in roof build-ups, not rain. Ripening rooms are small, sealed, and thermally heavy for their size; we position them inside the shell with their own envelope rules rather than treating the hall as one temperature.

Typical requirement set: humidity-managed roof build-up · ripening rooms as sealed sub-enclosures · intake-to-dispatch flow without temperature mixing · washdown-compatible finishes.
Frozen & Chilled Storage

Where this industry meets our Cold Storage type page

When the operation is pure storage — chilled 0–4 °C through deep-frozen −25 °C and below — the engineering moves fully into the territory of our Cold Storage Buildings page: panel classes, vapour sealing, thermal breaks at every penetration, and racking loads designed into the frame. This page covers the food-chain context; that page covers the storage engineering in depth.

Continue here: Cold Storage Buildings → for temperature-class engineering, panel specifications and cost logic.
Cold Chain Distribution

Docks with seals, a staged lobby, and trucks that cannot wait

Cold-chain distribution centres are the hand-off point: insulated hall on one side, dock bank on the other, and a temperature discipline maintained across dozens of daily door events. Dock seals and shelters, a staged temperature lobby between ambient and chilled zones, and dock counts decided by vehicle turns per hour — the same dock math as ambient logistics, run behind a thermally broken wall.

Typical requirement set: dock seals & shelters · thermal-break dock wall · staged lobby between zones · fast-roll doors with air curtains · 24/7 traffic laid out with the frame.

From operation to structure

How the process requirements above translate into engineering decisions.

If your operation… The structure must… Cost if decided late
Runs a daily washdown routine Carry galvanized / two-coat protection on all wet-zone steel, coved and sealed joints Recoating in year 2–3 costs multiples of specifying it
Holds −25 °C or colder Take 150–200 mm panels, oriented vapour barriers, thermal breaks at columns and doors Moving from 100 to 200 mm after panel order = new envelope
Has a hygiene audit regime Offer no ledges: flush connections, accessible voids, cleanable interfaces Failing audits stop production — the only cost that dwarfs steel
Concentrates tons (tanks, racking) Carry equipment reactions in the foundation design from day one Foundation upgrades under a live slab
Opens doors all day Protect zones with lobbies, seals and air curtains planned into the layout Energy loss billed monthly, forever

Building types this industry uses

Two families carry most food-chain projects — each linked below with how this industry actually uses it.

Primary

Cold Storage Buildings

Everything temperature-held: processing rooms, chilled stores, frozen chambers. Panel classes, vapour sealing and thermal-break details live on this page.

View building type →

Supporting

Steel Warehouses

Ambient zones of the food chain — dry-goods intake, packaging stores, dispatch halls that share the site with the cold core.

View building type →

Also built with: Workshops & Factories (processing halls with mezzanine process equipment)

Food & Cold Chain we have delivered

Every card opens a project page with the engineering numbers — span, temperature class, wind rating and delivery term.

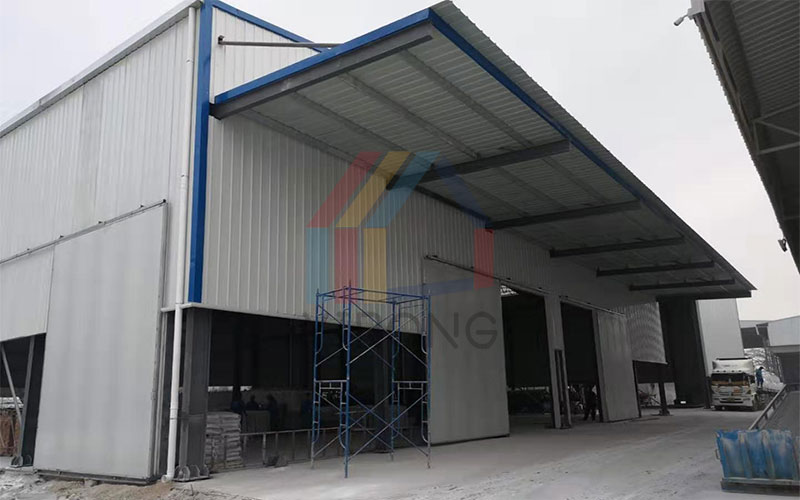
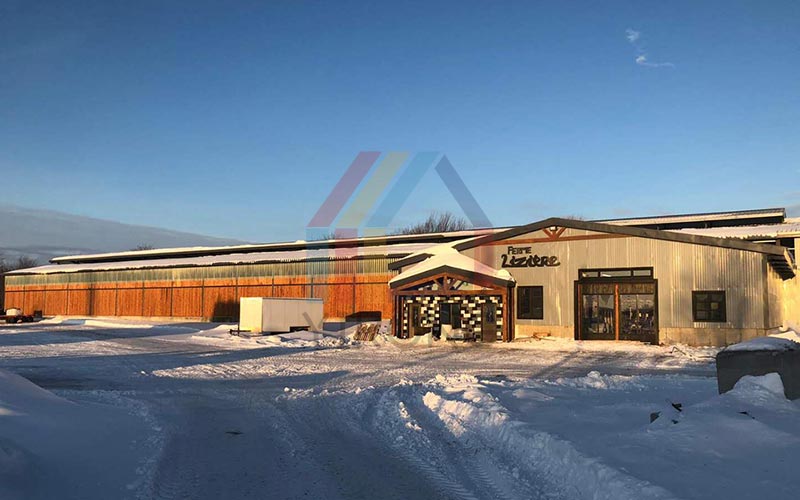
Canada Cattle Shed

Canada Cattle Shed

Grassland pasture belt, Alberta
3200㎡
Fiji Tea Processing Plant

Fiji Tea Processing Plant

Rabasa, North Island
750㎡
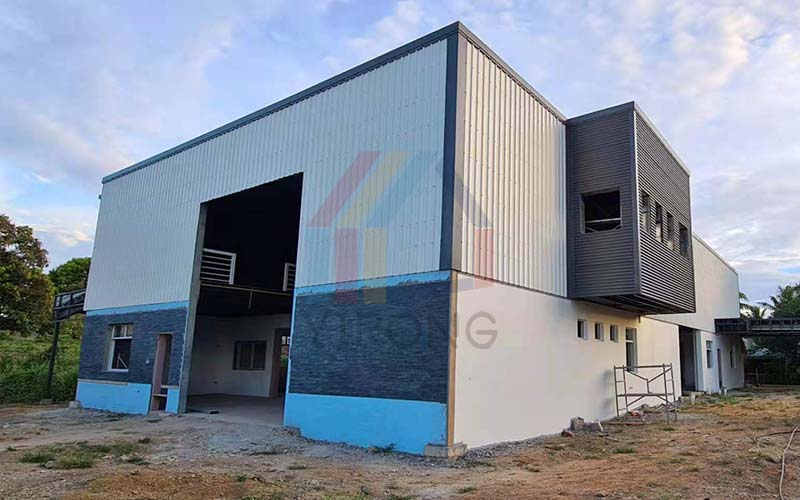
Thailand Lime Plant

Thailand Lime Plant

Phra Nakhon Si Ayutthaya
2160㎡

Questions food-chain buyers ask first

Chilled (0–4 °C) typically runs 100 mm; frozen (−18 to −25 °C) runs 150–200 mm depending on duty cycle and energy pricing. The decision variable is not comfort but condensation control — the panel class and the vapour-barrier orientation are one engineering decision, quoted together in a costed layout.

Yes — and most of ours do. The shell is one frame; inside it, processing rooms (3–8 °C) and frozen chambers (−25 °C) are separate sub-enclosures with their own envelope, doors and drainage. What cannot be shared is the panel class and the door strategy between zones — that is where costed layouts earn their keep.

By geometry first: flush connections, coved joints, no inaccessible cavities in wet zones. Coatings second: galvanized or two-coat systems on all steel in washdown areas, specified against the actual cleaning chemicals — we ask for the cleaning schedule as part of the design brief.

Material certificates, panel fire and food-safety compatibility documentation, structural calculations to destination code, and [CE / EN] marking where applicable — the pack ships with the building, not on request afterwards.

[3–4] months is typical for a [1,000–2,000] m² food-chain building, starting from your process flow and temperature schedule rather than from drawings. Port lead time and destination country add to this.